In the fast-paced world of logistics and supply chain management, the efficiency of operations can make or break business success. One often overlooked but vital component of this process is the humble pallet. Specifically, Grade A pallets stand out as a crucial asset for maximizing operational efficiency. These high-quality pallets are designed to endure rigorous use while maintaining structural integrity. By understanding the benefits and applications of Grade A pallets, businesses can significantly enhance their productivity and cost-effectiveness.
Understanding Grade A Pallets
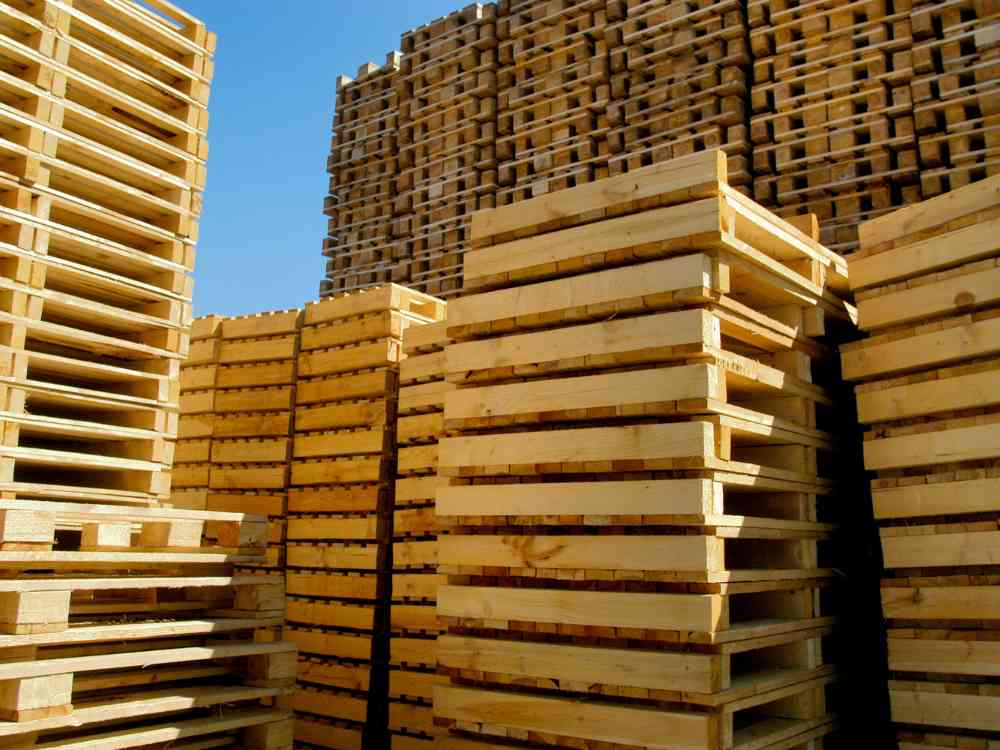
Grade A pallets are renowned for their superior quality and durability. These pallets are often made from high-grade materials and are meticulously inspected to ensure they meet stringent standards. Here are some key characteristics of Grade A pallets:
- Constructed from premium wood, often with minimal to no repairs.
- Uniform in size and appearance, ensuring compatibility with automated systems.
- Reliable structural integrity, ideal for heavy loads and repeated use.
- Compliant with industry standards, making them suitable for international shipping.
Benefits of Using Grade A Pallets
Incorporating Grade A pallets into logistical operations can yield numerous advantages:
Enhanced Efficiency
Grade A pallets contribute to smoother and faster warehouse operations. Their uniformity allows for seamless integration with automated pallet handling systems, reducing downtime and improving throughput.
Cost Savings
While the initial investment in Grade A Pallets may be higher, their durability and longevity translate into long-term savings. Reduced need for replacements and repairs means lower overall costs.
Improved Safety
Safety is paramount in any warehouse setting. Grade A pallets reduce the risk of accidents due to broken or faulty pallets. Their robust design ensures the secure transport and storage of goods.
Applications of Grade A Pallets
Grade A pallets are versatile and can be utilized in a variety of settings:
- Manufacturing Facilities: Suitable for carrying raw materials and finished goods efficiently.
- Retail and Distribution Centers: Ideal for transporting goods to and from storage areas.
- International Shipping: Compliant with global standards, making them perfect for cross-border logistics.
Choosing the Right Pallet Provider
When selecting a supplier for Grade A pallets, consider the following:
- Reputation and reliability of the supplier.
- Compliance with industry standards and certifications.
- Options for customization based on specific business needs.
- Availability of support and post-purchase services.
Conclusion
Maximizing efficiency in logistics and supply chain operations is crucial for maintaining a competitive edge in today’s market. By investing in Grade A Pallets, businesses can enhance their productivity, ensure safety, and achieve cost savings. Understanding their benefits and applications will empower companies to make informed decisions that align with their operational goals. As logistics continue to evolve, the role of high-quality pallets in facilitating smooth operations cannot be overstated.